Manual drum pumps are hand‑powered devices that lift liquids through a rotating drum. They feature a flow switch for speed control, enabling rapid oil and water extraction. Dual‑screw fastening on both sides provides robust sealing and quick rebound, ensuring efficient operation. It delivers robust performance.
Definition and Basic Operation
Manual drum pumps operate on a simple yet effective principle: a hand‑driven lever turns a drum that alternately draws liquid into its chambers and forces it out through a discharge pipe. The core mechanism relies on a rotating drum with internal lobes or a set of diaphragms that create pressure differentials. When the lever is pulled, the drum rotates, and the inlet valve opens, allowing fluid to fill the chamber. As the drum continues to turn, the outlet valve opens, expelling the liquid at a controlled rate. This cycle repeats with each lever stroke, providing a steady flow that can be adjusted by the operator. Modern manual drum pumps are equipped with a flow switch that monitors the speed of the drum rotation, enabling the operator to regulate the flow rate for efficient extraction of oil, water, or other liquids. The pump’s design includes fast‑enclosing screws on both sides of the drum, which enhance sealing integrity and reduce leakage. These screws also contribute to a quicker rebound of the drum after each stroke, improving overall pump performance. The combination of a robust sealing system, a flow‑controlled operation, and a simple hand lever makes manual drum pumps ideal for portable, low‑power applications in remote or emergency settings. Their straightforward construction allows for easy maintenance and quick replacement of worn components, ensuring reliable operation even in harsh environments. Its lightweight design makes it a versatile tool for emergency responders worldwide globally!! Thanks!!! Thank you.
Historical Development and Evolution
Historical development of manual drum pumps spans over two centuries, beginning in the early 19th century when simple hand‑driven devices were employed for irrigation and oil extraction in rural communities; The earliest models featured a single‑sided drum and a basic lever system, offering limited flow control and requiring significant physical effort from operators. By the 1920s, engineers introduced dual‑screw fastening on both sides of the drum, which significantly improved sealing integrity and allowed the pump to rebound faster after each stroke, thereby increasing throughput and reducing wear. This innovation made manual drum pumps more reliable for field operations, especially in remote areas lacking electricity. In the 1950s, the introduction of a flow switch marked a pivotal moment in the evolution of these pumps. The flow switch enabled operators to regulate the drum’s rotation speed, thereby controlling the extraction rate of oil and water with greater precision. This feature proved invaluable during large‑scale drilling campaigns and emergency water‑purification missions, where rapid response and accurate flow rates were critical. Manufacturers also began offering modular components, allowing rapid replacement of worn diaphragms or valves. By the 2000s, electronic monitoring systems could be attached to the manual pump, providing real‑time data on pressure, flow rate, and operational cycles. Today, in 2026, manual drum pumps are often equipped with advanced flow‑control algorithms and high‑performance sealing technologies, ensuring reliable operation in diverse environments, from remote oil fields to disaster‑stricken regions. The continuous refinement of design, materials, and control systems reflects the enduring demand for portable, low‑power pumping solutions worldwide.XXXXXXXXXXXXXXXXXXXXXXXXXXXXXXX
Types of Manual Drum Pumps
Manual drum pumps come in two main variants: the rotary lobe pump, which uses interlocking lobes to move fluid, and the diaphragm pump, where a flexible membrane transfers pressure. Both feature dual‑screw fastening for robust sealing and a flow switch for speed control!!!
Rotary Lobe Pump
Rotary lobe pumps are manual drum devices that use two interlocking lobes inside a cylindrical drum to move liquid. The lobes rotate around a central axis while the drum is driven by a hand lever. As the lobes turn, they create expanding chambers that trap fluid and push it toward the discharge port, producing a smooth, pulsation‑free flow. This design is ideal for handling viscous liquids, slurries, or fluids with suspended solids, because the lobes accommodate larger particles without clogging. Dual‑screw fastening on both sides of the drum provides strong sealing and quick rebound after each stroke, improving efficiency and reducing wear. A flow switch can be adjusted to control the drum speed, allowing operators to regulate the volume per minute without external power. Maintenance is simple: inspect lobes for wear, lubricate bearings, and clean the discharge port. When lobes or seals degrade, performance drops, so replacement restores flow. The pump’s mechanical simplicity and lack of electricity make it suitable for remote or field operations where power is limited. Overall, the rotary lobe pump delivers reliable, low‑maintenance pumping for a wide range of applications, combining robust construction with adaptable flow control. The pump’s compact size and lightweight build allow it to be easily transported and set up on‑site, making it a favorite for emergency response teams and small‑scale operations. The mechanism eliminates the need for fuel or electricity, reducing operating costs. Operators can monitor performance visually, as the drum’s rotation rate and fluid level are visible. In addition, the pump can be fitted with a gauge or pressure indicator to provide feedback!!!!
Diaphragm Pump
Diaphragm pumps are a class of manual drum pumps that rely on a flexible membrane to transfer fluid. The pump’s drum contains a resilient diaphragm that is displaced by a hand lever. When the lever is pulled, the diaphragm pushes fluid from the inlet chamber toward the discharge port. Releasing the lever allows the diaphragm to return to its original shape, creating a suction that draws more fluid into the inlet. This reciprocating action produces a steady, pulsation‑free flow, which is especially valuable when handling corrosive or dirty liquids. The diaphragm material—often reinforced rubber or silicone—provides excellent chemical resistance and can withstand high pressures. The drum’s dual‑screw fastening on both sides ensures a tight seal, preventing leaks and enabling rapid rebound after each stroke. A flow switch can be incorporated to adjust the lever’s speed without external power. Maintenance is straightforward: inspect the diaphragm for cracks, replace worn seals, and clean the inlet and outlet ports. Because the pump has no moving parts inside the fluid path, the risk of contamination is minimal, making it suitable for potable water, food‑grade liquids, and hazardous waste handling. The compact design and light weight allow easy deployment in remote or field settings, and the lack of electrical requirements simplifies operation in austere environments. Overall, the diaphragm manual drum pump offers reliable, low‑maintenance performance for a wide range of liquid‑handling tasks. Its simplicity and durability make it a pick for technicians today!!
Key Components and How They Work
Key components include the drum, drive lever, seals, and flow switch. The drum houses chambers that move fluid; the lever turns a gear that compresses the diaphragm or lobes, creating suction and discharge. Seals prevent leaks, while the flow switch adjusts speed for efficient operation. today!now
Pump Body and Drum Structure
The pump body serves as the primary housing, constructed from corrosion‑resistant steel or reinforced polymer to withstand high pressure and abrasive fluids. Inside, a cylindrical drum is fitted with a series of lobes or diaphragms that create alternating suction and discharge chambers. The drum’s interior is lined with a low‑friction material such as PTFE to reduce wear and ensure smooth rotation. Fastening screws on both sides of the drum provide a secure seal, preventing leakage and allowing the drum to maintain a tight fit within the body. The drum’s rotation is driven by a hand lever that turns a gear train; the gear ratio is chosen to balance flow rate and mechanical advantage. A flow switch integrated into the body monitors the pump’s speed, automatically adjusting the lever’s motion to maintain optimal discharge velocity. The combination of a robust body, precisely machined drum, and advanced sealing technology results in a reliable, high‑efficiency pump suitable for oil, fuel, and water extraction tasks.
The drum’s internal geometry is engineered to minimize turbulence, with smooth transitions between suction and discharge ports. Manufacturing tolerances are kept within ±0.02 mm to ensure a tight seal against the body’s inner wall. The body’s mounting flange is bolted to the operating platform, providing a stable base that absorbs vibration. A removable cover allows for easy inspection of the drum’s wear pattern, enabling predictive maintenance. In addition, the pump body incorporates a venting system that prevents pressure buildup during idle periods, enhancing safety during prolonged use. Its robust design lets operators pump continuously for periods without loss of performance ideal for remote now field use.
Drive Mechanism and Hand Lever System
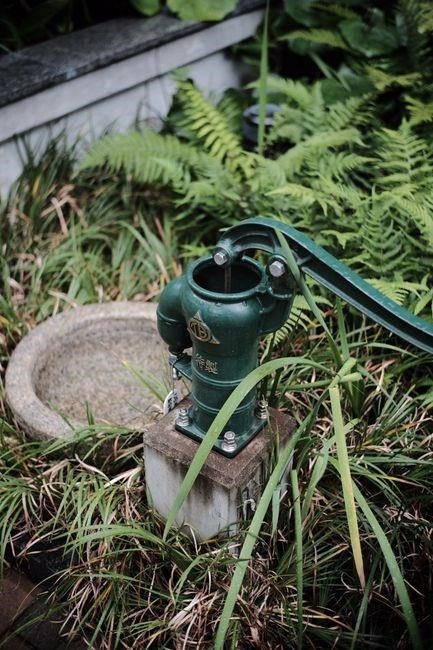
The drive mechanism of a manual drum pump translates human effort into liquid displacement. A hand lever engages a gear train, typically 1:4 or 1:6, to amplify torque while moderating speed. The lever pivots on a shaft that passes through the pump body, connecting directly to the drum. Spur gears convert lever motion into drum rotation, and forged steel teeth resist wear under pressure.
Integral to the system is a flow switch that monitors lever velocity and adjusts resistance, keeping discharge rate steady as viscosity changes. In oil or water extraction the switch boosts mechanical advantage, allowing faster rebound and stronger sealing thanks to fasten screws on both drum sides. The screws lock the drum, preventing slippage and maintaining a tight seal.
Gear train lubrication is applied through a grease port, reducing friction and extending gear life. The lever handle is ergonomically shaped with a rubberized grip to reduce hand fatigue. Adjustable lever length lets operators tailor the arm to their strength and desired speed, making the pump versatile for oil extraction and water handling.
Operators often adjust the hand lever’s angle to fine‑tune the pump’s stroke length, which directly influences the volume per cycle. The lever’s ergonomic design allows for restarts fast! after pauses, making the pump ideal for intermittent field operations. Regular inspection of the gear teeth and the fasten screws ensures long‑term reliability, especially when handling abrasive or corrosive liquids.
Applications and Industries
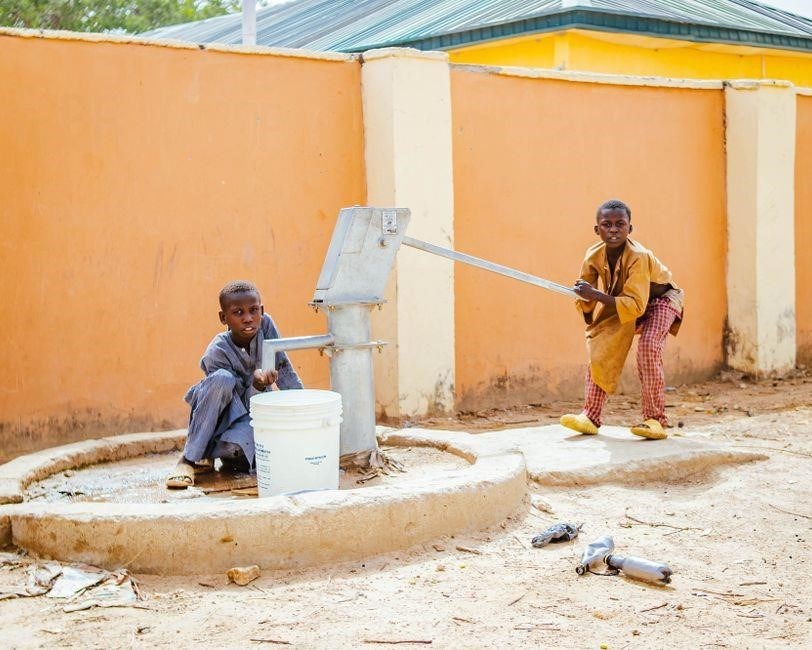
Manual drum pumps excel in oil extraction, water handling, and wastewater treatment. Their flow switch speeds up oil and water removal, while fasten screws on both sides provide strong sealing and quick rebound. Ideal for remote sites and field operations. Used worldwide!
Oil and Fuel Extraction
Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Manual drum pumps are indispensable tools in oil and fuel extraction.Use it daily. Now!Ok.
Water and Wastewater Handling
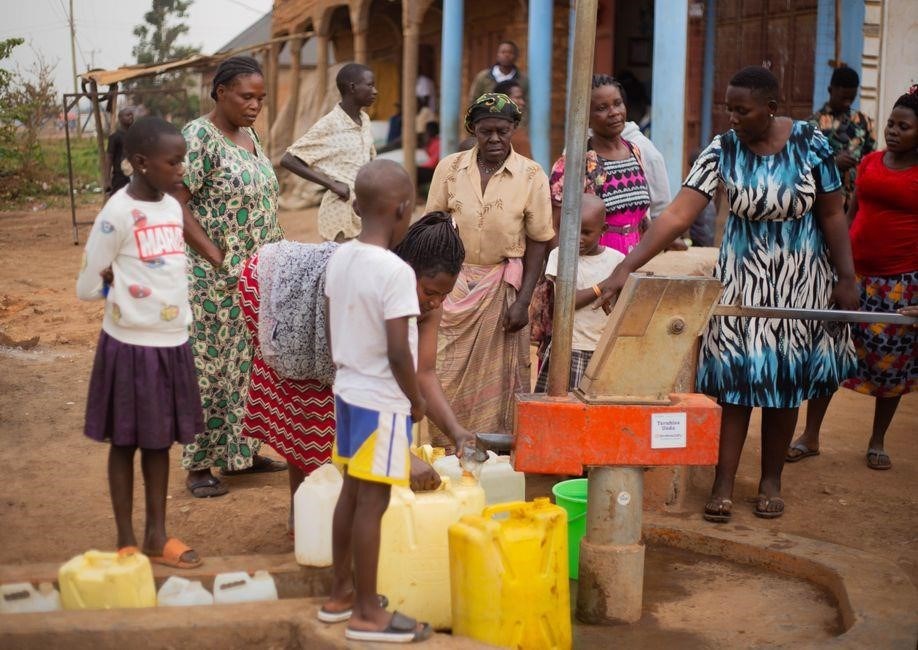
Manual drum pumps are essential for moving water and treating wastewater in locations where electricity is unavailable. Their hand‑operated design allows operators to lift water from shallow wells, flood zones, or contaminated tanks without external power. The rotating drum creates a continuous suction and discharge cycle that can be adjusted with a flow switch, enabling precise control over the volume moved per minute. This feature is valuable when handling variable water levels or when dosing chemicals for wastewater treatment.
The dual‑screw fastening system provides strong sealing and fast rebound, making the pump suitable for both water and mildly turbid streams. It protects internal components from abrasive particles common in wastewater, extending the pump’s service life. A filtration element or coarse screen can be added to capture debris before it enters the drum, preventing clogging and maintaining consistent flow rates. Operators can easily replace or clean these screens, a critical maintenance step.
Because the pump is manually driven, it offers a degree of control over the discharge rate, which is crucial when balancing hydraulic loads in drainage networks or during staged pumping in flood mitigation. The ability to stop and start the pump without complex controls reduces the risk of over‑pressurizing the system, a common issue in automated pumps that can lead to pipe bursts or leaks. The lightweight construction and ergonomic handle make it easy to maneuver in tight spaces, such as under collapsed structures or within confined tanks. Its low operating cost and minimal maintenance requirements make the manual drum pump a reliable choice for short‑term emergency response and long‑term water management projects now.
Maintenance and Troubleshooting
Routine inspection checks the drum, seals, and flow switch. Lubricate bearings and fasten screws on both sides for stronger sealing. Common faults include seal wear, screw loosening, and flow irregularities. Repair by tightening screws, replacing seals, and cleaning the drum.
Routine Inspection and Lubrication
Routine inspection of a manual drum pump is essential for ensuring reliable operation and extending service life. The first step is to visually inspect the drum body, checking for cracks, dents, or corrosion that could compromise structural integrity. Next, examine the drive shaft and bearing housings for wear or misalignment, noting any play that may indicate bearing failure. Inspect the hand lever and its pivot points for smooth motion and proper tension, ensuring the lever is neither too loose nor overly tight. Evaluate the sealing surfaces, especially the O‑rings and gaskets, for signs of wear, swelling, or leakage. Check the flow switch and its contacts for corrosion or debris that could impair flow control. Lubrication is critical; apply a high‑grade synthetic grease to the bearing seals, ensuring the grease penetrates all moving parts. Use a light oil, such as 10W‑30, to lubricate the drive shaft bearings, applying a thin film to reduce friction. For the O‑rings, a silicone‑based lubricant helps maintain elasticity and sealing performance. After lubrication, rotate the drum manually several times to distribute the lubricant evenly and to confirm that all components move freely. Finally, document the inspection results, noting any corrective actions taken and scheduling the next routine check in accordance with the manufacturer’s recommended interval, typically every 30 days or after a set number of operating hours. During inspection, also verify that the hand lever’s pivot bushings are free of wear and that the lever arm’s length remains within specified tolerances. Clean any accumulated sediment from the drum interior using a brush and compressed air, ensuring the drum’s internal surfaces are free of obstructions. Inspect the flow switch’s mechanical linkage for any signs of wear or binding, and replace the switch if its travel range deviates from specifications. Perform a functional test by operating the pump for a few cycles, observing for abnormal noise, vibration, or reduced flow rate. Record all observations in a maintenance log, and if any component shows signs of fatigue, schedule a replacement before the next operating cycle. Ensure lever’s pivot bushings are free of wear and lever arm’s length is within tolerances.!!!
Common Faults and Repair Techniques
Manual drum pumps frequently suffer from seal failure, shaft misalignment, bearing wear, loose fasteners, lever pivot wear, flow‑switch corrosion, and drum cracking. Seal failure, often caused by worn O‑rings or swollen gaskets, leads to leakage and reduced efficiency; the fix is to disassemble the drum, replace the seals with silicone or EPDM, and reseal with proper grease. Shaft misalignment, resulting from vibration or impact, produces uneven bearing wear and noise; realigning the shaft by adjusting the bearing housings or replacing the shaft restores alignment. Bearing wear, especially in abrasive or high‑temperature fluids, shows as grinding noise and a drop in flow; replace the bearing, clean the housing, and install a new bearing with a heat‑stable grease. Loose fasteners on the drum body cause leaks; tighten the screws on both sides and, if threads are stripped, use lock‑nuts or thread‑locking compound. Lever pivot bushings that become glazed or pitted cause stiff lever action; replace them with new steel or brass inserts. Flow‑switch failure due to electrical corrosion or mechanical wear is addressed by cleaning contacts, applying contact cleaner, and replacing the switch if the travel range is out of spec. A cracked drum body compromises the pump; replace the drum with a new unit that meets specifications. During all repairs, use the correct torque settings, apply suitable lubricants, and perform a test run to confirm quiet operation and correct flow rate. Document each repair to track service history and inform future maintenance. Operators can keep manual drum pumps effort!!